Operation and process boundary
Handle, tape, inspect or package cable at a defined process point.
| Incoming material | Machine operation | Output |
|---|---|---|
| Wire or cable at the selected stage | Handling, inspection & finishing | A checked, taped or packaged product for the next operation |
Each supporting unit has a defined duty. Taping is not a complete braiding package, in-line checks do not replace final cable testing, and cable coiling or cutting does not include plug or connector assembly.
First selection check: Operating task, cable dimensions, reel or coil format
Choose the function your line needs.
Match each supporting unit to a defined process position, cable size and machine interface.
Taping equipment
Specified single or double-layer tape applications
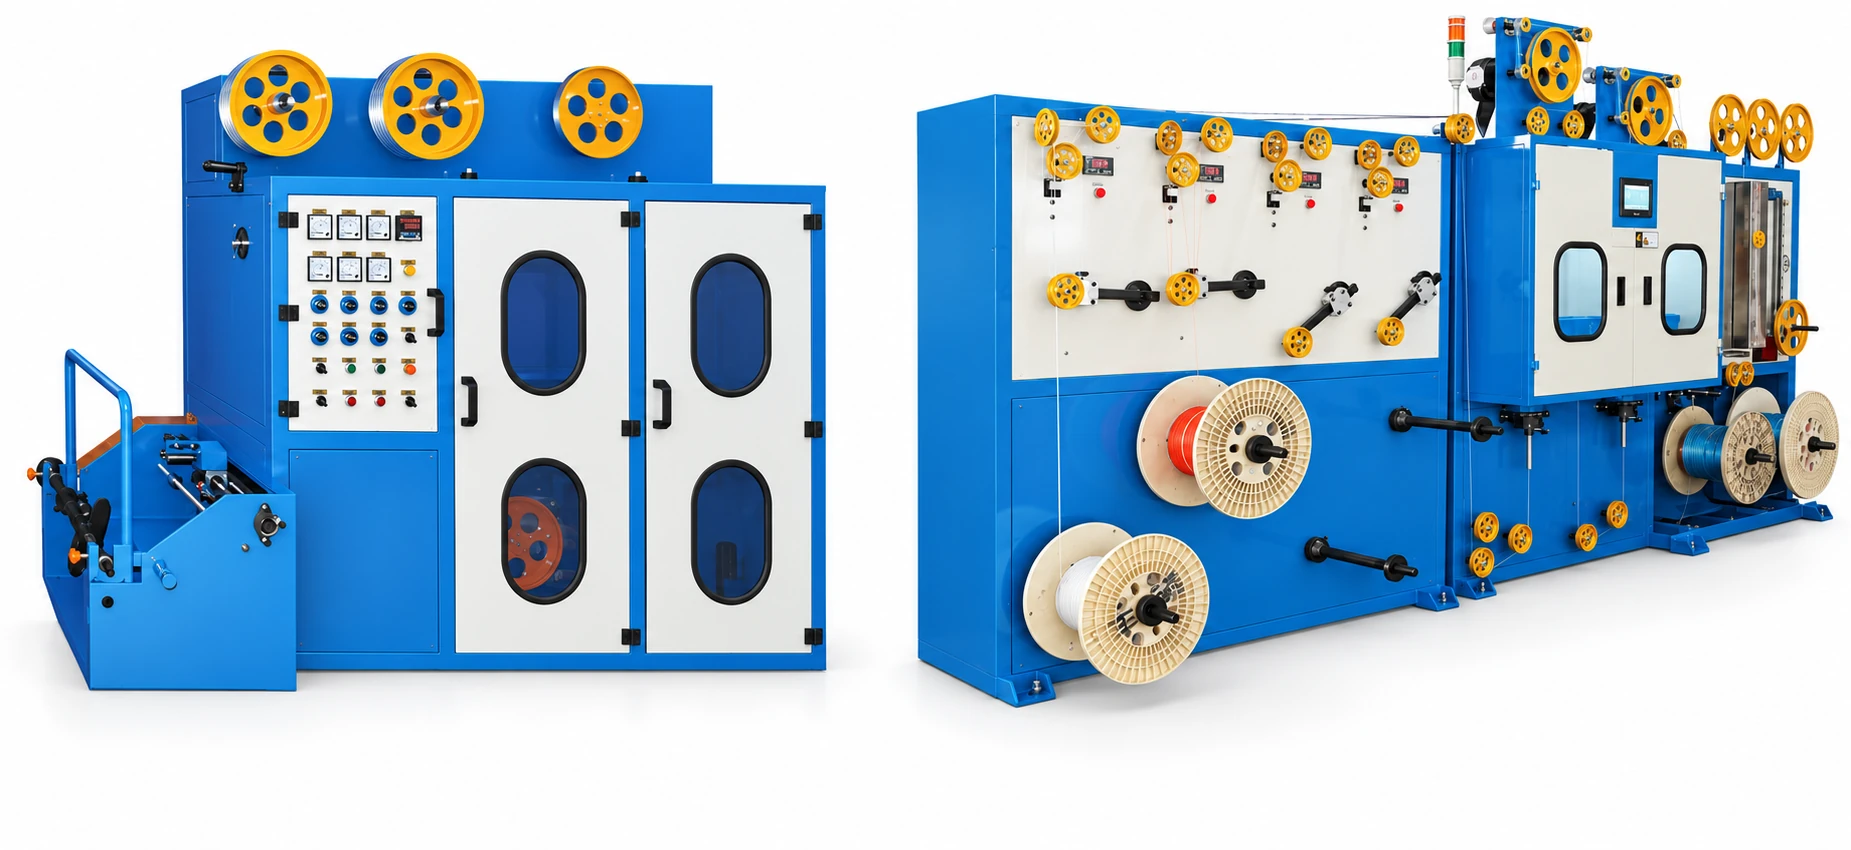
| Input | Operation | Output |
|---|---|---|
| Wire or cable core and specified tape | Taping | Core with the specified tape layer |
Review for the catalogue’s continuous cable-taping operations, with the required tape arrangement and overlap.
Selection inputs: Tape material, width, overlap, cable size and process position.
Confirm longitudinal or concentric taping as required. This is not a specification for handheld harness-taping tools.
Pay-off & take-up
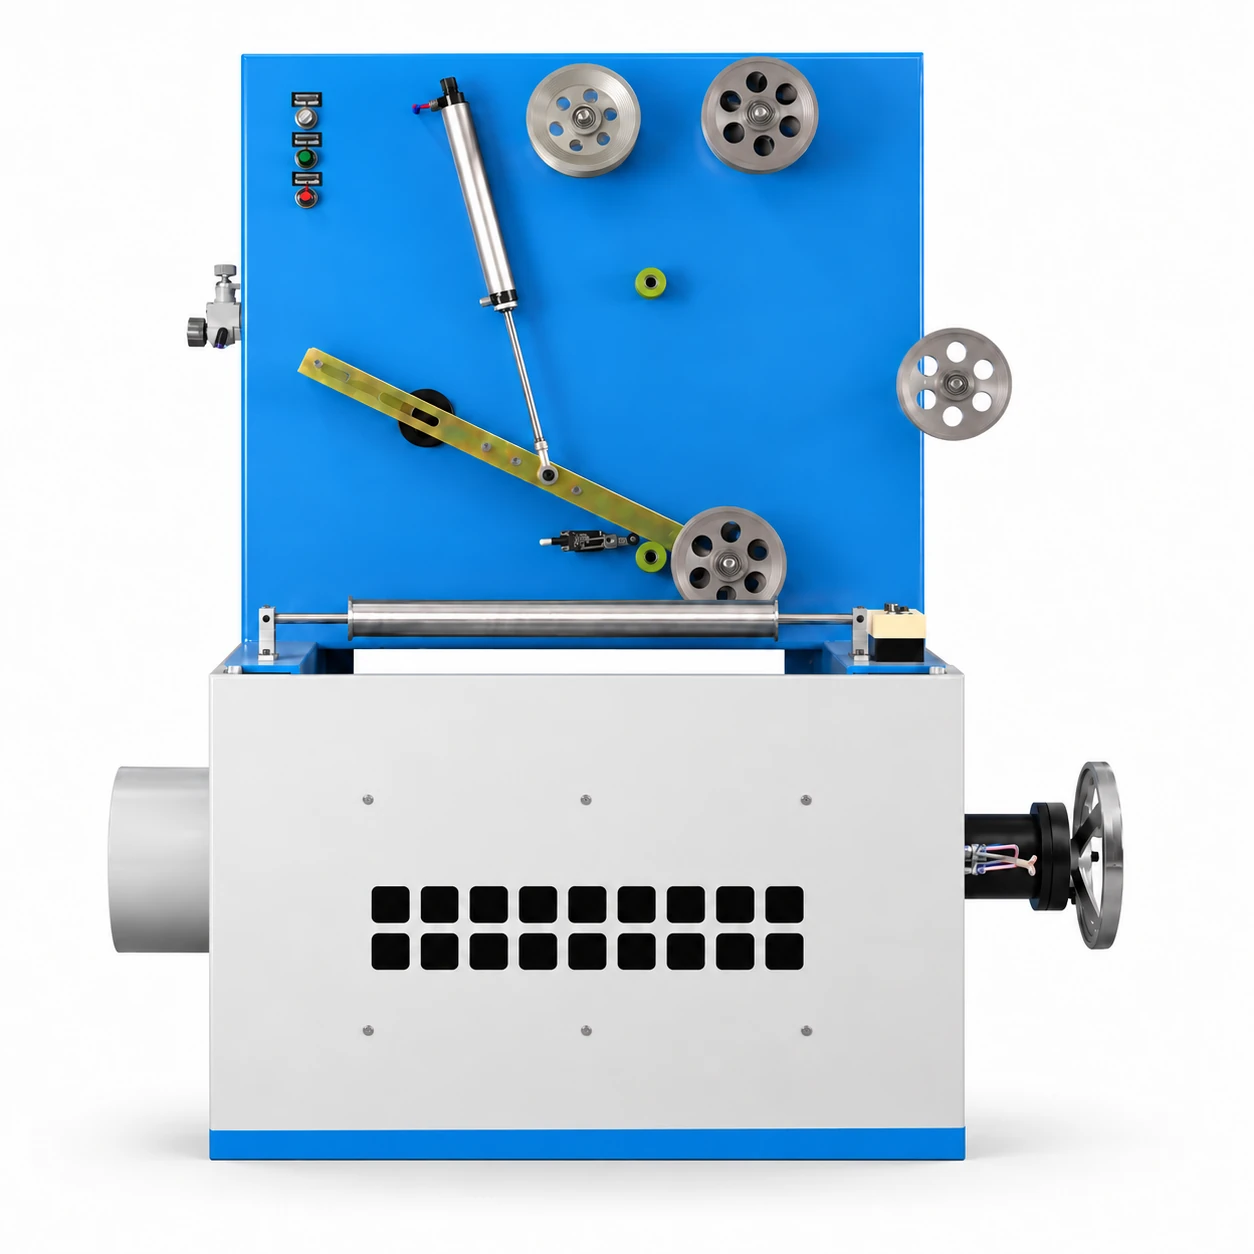
Coordinated material supply and collection
| Input | Operation | Output |
|---|---|---|
| Supply reel / material from the process | Pay-off / take-up | Controlled feed / collected cable reel |
Review when material supply or collection must fit an existing machine, reel format and tension arrangement.
Selection inputs: Reel dimensions, loading, tension and line interface.
Pay-off and take-up need their own loading, tension and control specifications. Packaging model values do not apply.
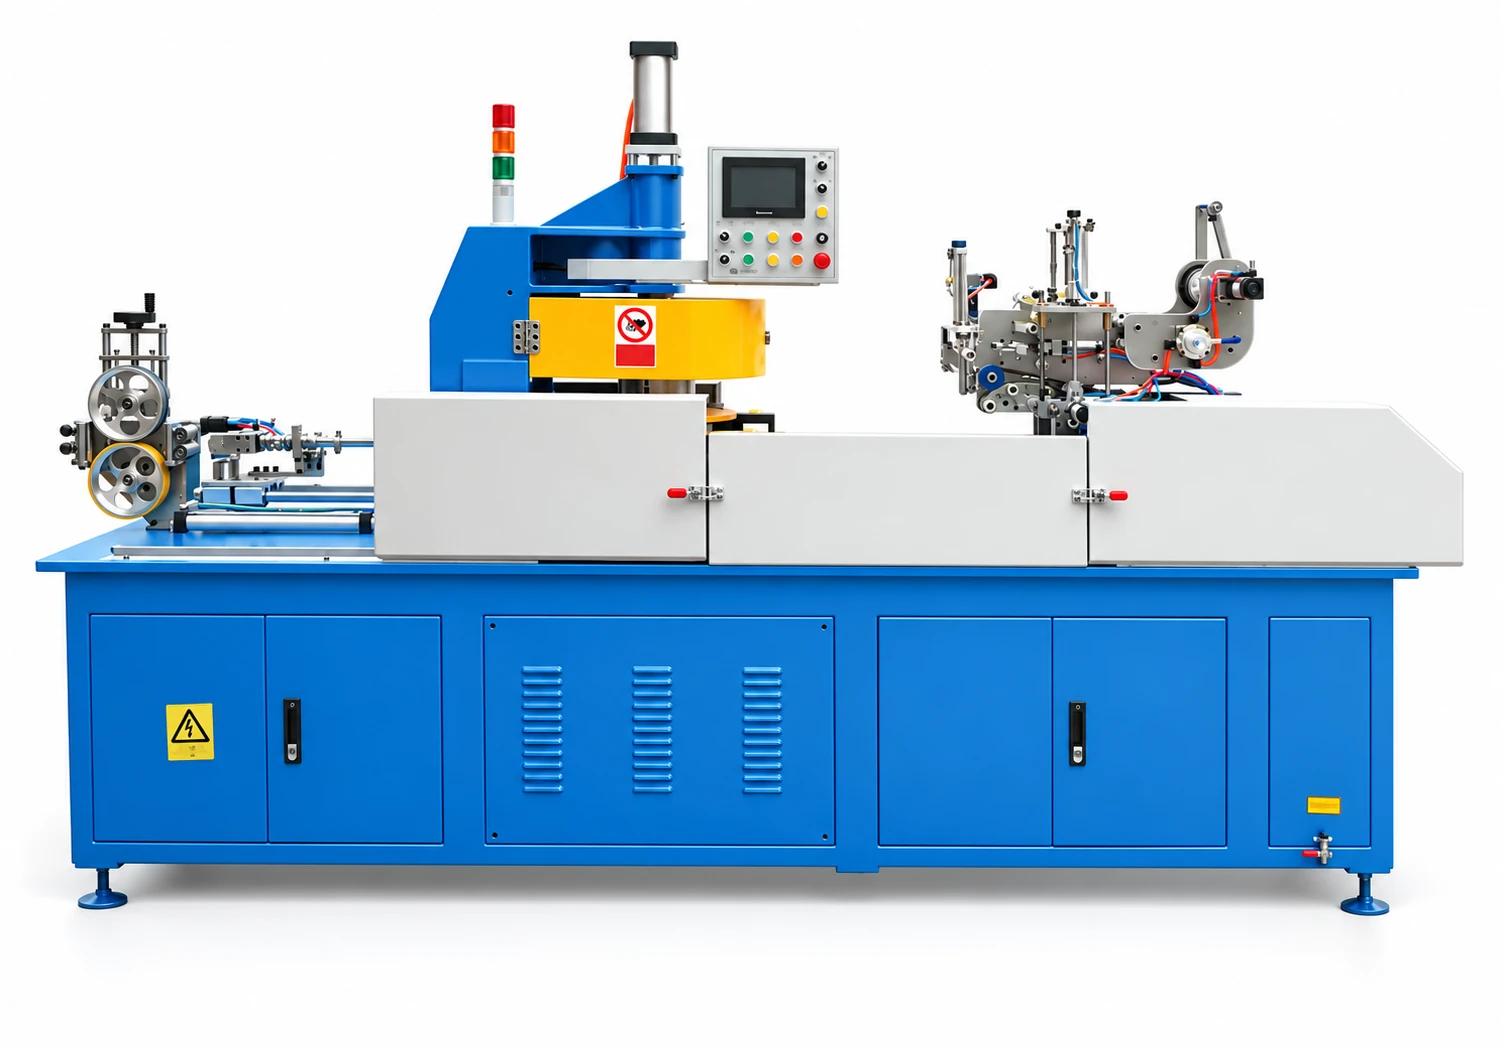
Coiling, wrapping & cutting
Finished cable handling and packaging
| Input | Operation | Output |
|---|---|---|
| Finished cable | Coiling and wrapping | Cable coil in the required package |
Review when the finished cable will be coiled and wrapped. Confirm coil geometry and cable flexibility together.
Selection inputs: Cable size, target length, coil format and packaging requirements.
PYJB1246 / PYJB1860 cover coiling and wrapping only. Separate cutting, labeling and handling requirements need confirmation.
Reference tables: Automatic PLC coiling & wrapping.
Spark testing & diameter measurement
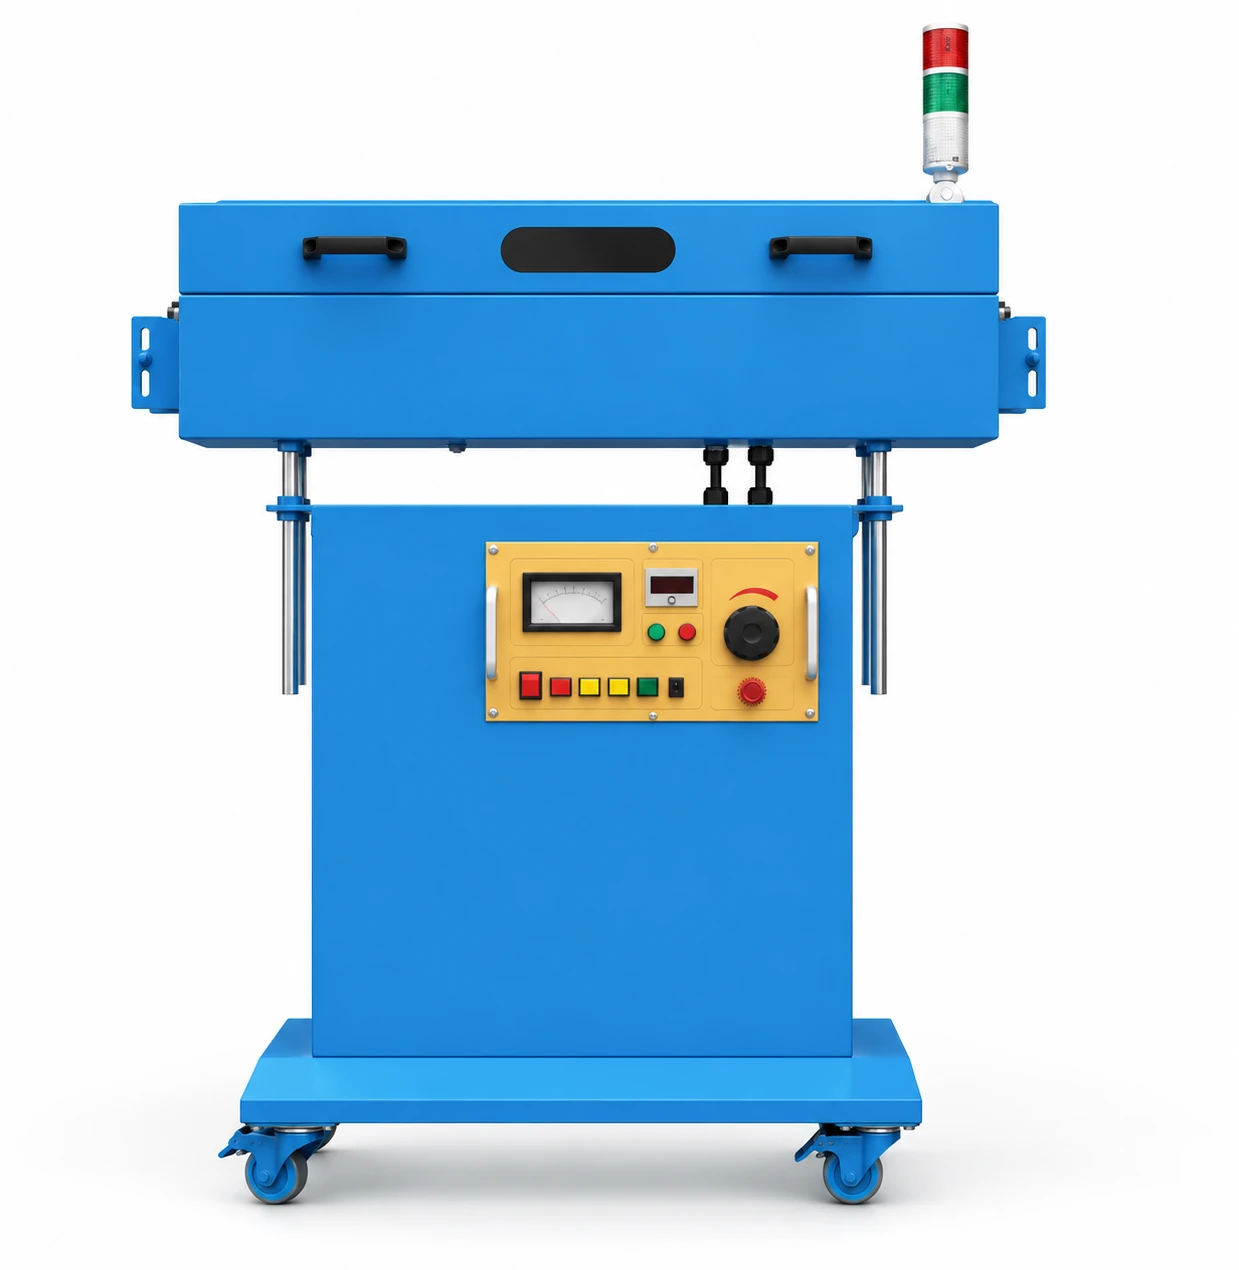
Inspection at the selected production stage
| Input | Operation | Output |
|---|---|---|
| Cable at the specified process stage | Spark test / diameter measurement | In-process inspection result |
Review the inspection purpose and position before choosing the tester or measuring device.
Selection inputs: Cable dimensions, process location and the required inspection method.
Device range and integration need a separate review. In-line checks do not replace finished-cable testing.
Product handling and connection to your line
| Selection priority | What to review |
|---|---|
| Define the finished package | Cable diameter alone is not enough for a coiler. Specify the coil inside and outside diameters, height, length and wrapping requirements. |
| Review the line interface | A pay-off, take-up or inspection unit must work with the existing cable path, tension and control arrangement. Include the main machine details when planning a retrofit. |
| Distinguish process and final testing | Spark testing and diameter measurement address defined production checks. The finished cable still needs its own validation plan for the intended application. |
Cable coiling and wrapping: reference configurations
PYJB1246 and PYJB1860 describe automatic cable coiling and wrapping. Pay-off, take-up, taping and inspection units need separate duty and interface specifications.
Automatic PLC coiling & wrapping
| Model | Wire Ø (mm) | Max. coil OD (mm) | Coil ID (mm) | Traverse height (mm) |
|---|---|---|---|---|
| PYJB1246 | 1–6 | 400 | 140–200 | 40–100 |
| PYJB1860 | 2–16 | 600 | 200–300 | 60–180 |
Confirm cable flexibility, coil length and packaging requirements. Coiling speed and completed packages per minute are different measures.
Configuration sequence
| Stage | What to confirm |
|---|---|
| Identify the interface | Map each supporting unit to a defined point in the process. |
| Define its task | Specify the tape, reel, measurement or finished package required. |
| Match the main line | Review dimensions, tension, line control and operating requirements. |
| Plan the workflow | Check access, operator handling and movement between process stages. |
Choose the purchase situation
Connecting material handling
A main machine needs compatible supply, collection or tape handling.
Review pay-off, take-up or taping against the cable path, tension, reels, tape and main-machine controls.
Provide the connection-point drawing and details of the adjacent machine.
Adding an in-line check
A defined production stage needs spark testing or diameter measurement.
Specify the purpose, product dimensions, position and the process response required.
Describe the check required and the existing line interface.
Preparing the finished package
Cable must be coiled, wrapped or cut for the next operation or shipment.
Review cable flexibility, finished length, coil dimensions, loading and wrapping requirements.
Provide the package specification and how cable arrives from the main process.
Interfaces with the surrounding process
| Interface | Review requirement |
|---|---|
| Main machine to supporting unit | Match cable dimensions, operating conditions, tension, centreline and the mechanical connection. |
| Controls and line response | Confirm the control interface, signal requirements and what happens when the unit or main line stops. |
| Finished package to handling | Agree reel or coil dimensions, cable length, wrapping and operator access before comparing equipment. |
Equipment package and responsibilities
Agree in the equipment package
- The required taping, handling, inspection or finishing unit
- Cable path, reel dimensions and tension requirements
- Line control and mechanical interfaces
- Coil, cut-length or wrapping format
Confirm separately
- Existing machine information and retrofit access
- Consumable tapes, wrapping materials and reels
- Label content and finished package acceptance requirements
Review the technical proposal
Does the supporting unit fit the product and the machines on both sides?
| Review item | Compare on the same basis | Requested evidence |
|---|---|---|
| Defined duty | Distinguish paying off, taking up, taping, inspection, coiling and cutting. Each has a different selection basis. | A duty schedule stating what each unit accepts and delivers. |
| Mechanical fit | Confirm cable dimensions, reel geometry, load handling and the available operating space. | Reel/product drawings and the mechanical interface to the retained line. |
| Controls & quality | Agree tension, speed coordination, signals and required checks; an in-line device does not replace every finished-cable test. | An interface/responsibility list and a validation method for the unit’s specific duty. |
| Package & handover | Identify guarding, accessories, consumables, documentation and service arrangements relevant to the selected unit. | An itemised scope and the agreed installation/start-up responsibilities. |
What changes the quotation scope?
The unit’s duty, product and reel range, control integration, measurement needs and accessories change the package.
Cable production applications
LAN & Data Cable
Apply specified tapes at the selected LAN cable assembly stage.
Confirm tape layers and position. A braiding stage needs its own scope.
LAN & Data Cable production line
Solar Cable
Prepare the agreed coil package after solar-cable processing.
Confirm cable flexibility, coil dimensions, length and the required finished-product checks.
Power & Building Cable
Prepare coils for suitable building-wire or power-cable sizes.
Check the listed coiling range and package; larger cable may need a different reel-handling arrangement.
Power & Building Cable production line
Power Cord
Package bulk power-cord cable after insulation, assembly and sheathing.
Coiling and cutting concern the cable. Plug molding and termination are outside this scope.
Coaxial Cable
Review tape application within the specified coaxial shield structure.
Confirm tape suitability, layer position and separate braiding responsibilities.
USB & Data Cable
Review specified tapes around the data-cable core or pairs.
Define each tape and shield layer; braiding, connectors and final assembly remain separate scope decisions.
USB & Data Cable production line
Frequently asked questions
Can auxiliary equipment be supplied for an existing line?
Share the current equipment and the interface requirements. The supporting unit needs to fit the actual cable dimensions and operating conditions.
Can a coiling machine be selected from cable diameter alone?
Diameter is only one input. Cable flexibility, coil dimensions, length, handling and packaging needs also matter.
Does in-line inspection replace all finished cable testing?
No. In-line inspection serves a defined process purpose. Finished cable verification and applicable test requirements should be established separately for the product.
Can coiling speed be used as packaging output?
No. Coiling length, loading, wrapping and handling all affect completed packages. Define the coil length and finished package before comparing output.
What information is needed for an existing-line retrofit?
Provide the main machine details, cable range, operating speed, reel dimensions, control interface and available space. Include photos or drawings of the proposed connection point.
Prepare the equipment requirements
| Requirement | Information to provide |
|---|---|
| Product | Cable or conductor dimensions, material and handling constraints. |
| Operating task | Taping, coiling, cutting, inspection or reel handling requirements. |
| Line compatibility | Existing equipment, interface details and process position. |
| Finished package | Reel or coil dimensions, length and wrapping requirements. |
For a single machine, a line upgrade or a new production line, prepare the cable drawing, input and output requirements, reels and process interfaces.
The current project form prepares a local downloadable brief; it does not send an inquiry.