Skip to content
PINYANG MACHINERY

Production line configuration

Power Cord Cable Production Line

Plan flexible-conductor bunching, core insulation, cable assembly, sheathing and finishing for the cable used in power cords.

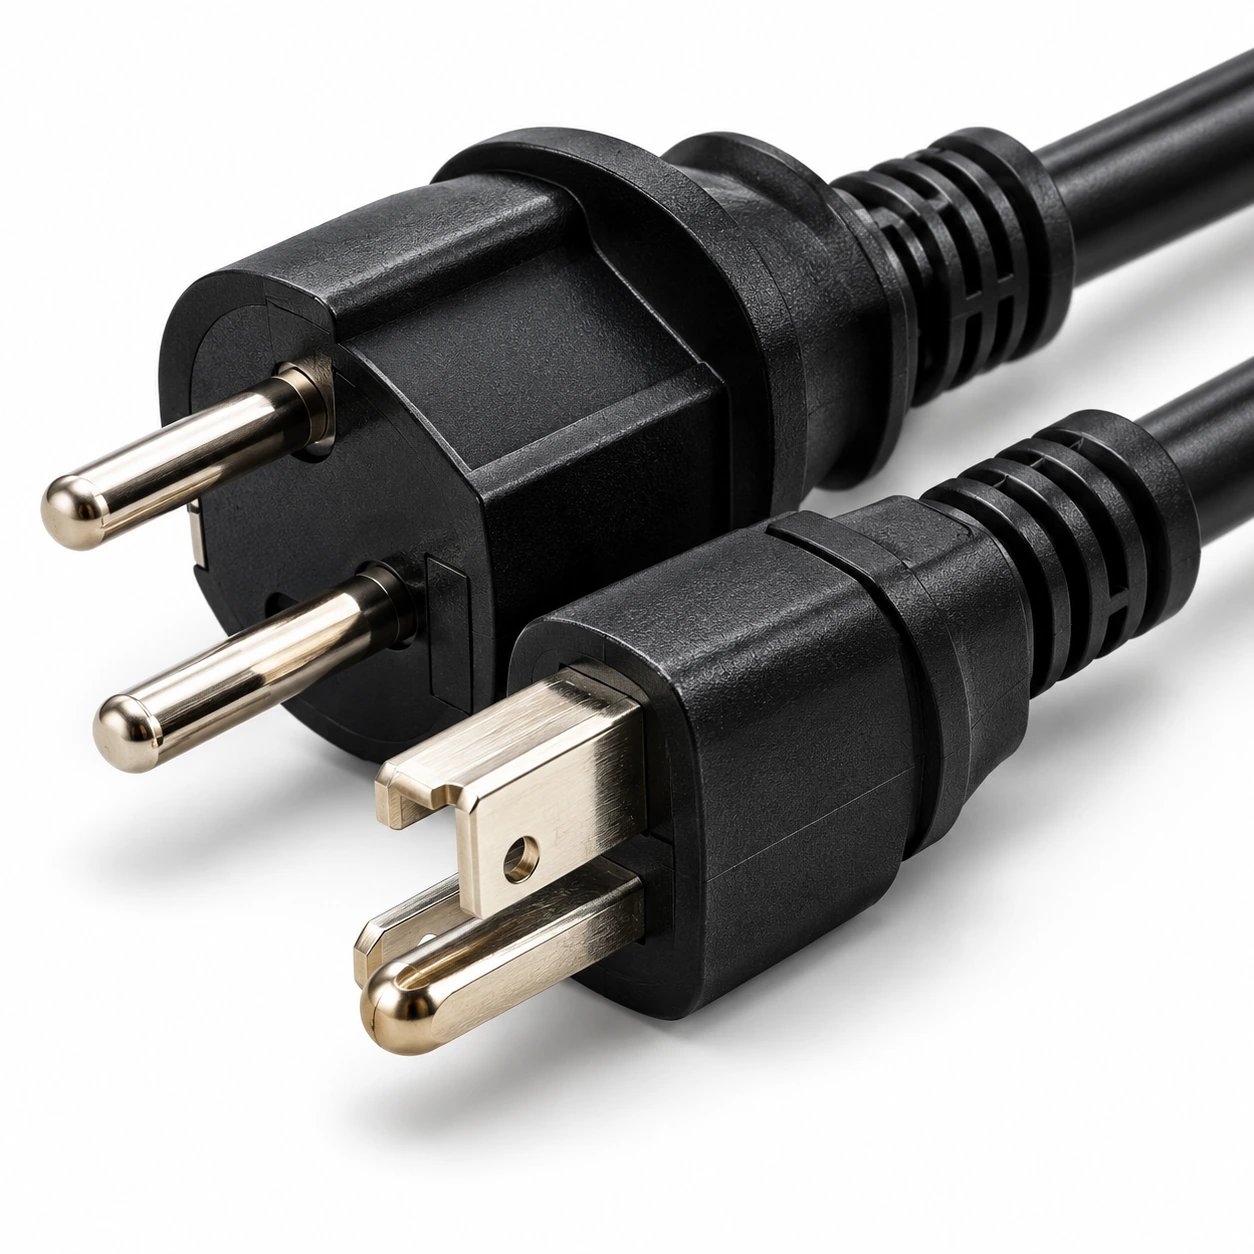
Power cord illustration with molded plugs
Power CordApplication illustration

Define the cable you want to produce

Core count, conductor cross-section, insulation and sheath materials, finished diameter, target length and output.

Bunched conductor → insulated cores → assembly → sheath → cutting or coiling

Indicative process route; confirm against your cable drawing.

Selection priority

Core count, flexibility and finished dimensions

Choose where your production begins

Choose where cable manufacture begins and where your finished package ends. The cable-making scope and plug or termination work should be costed and accepted separately.

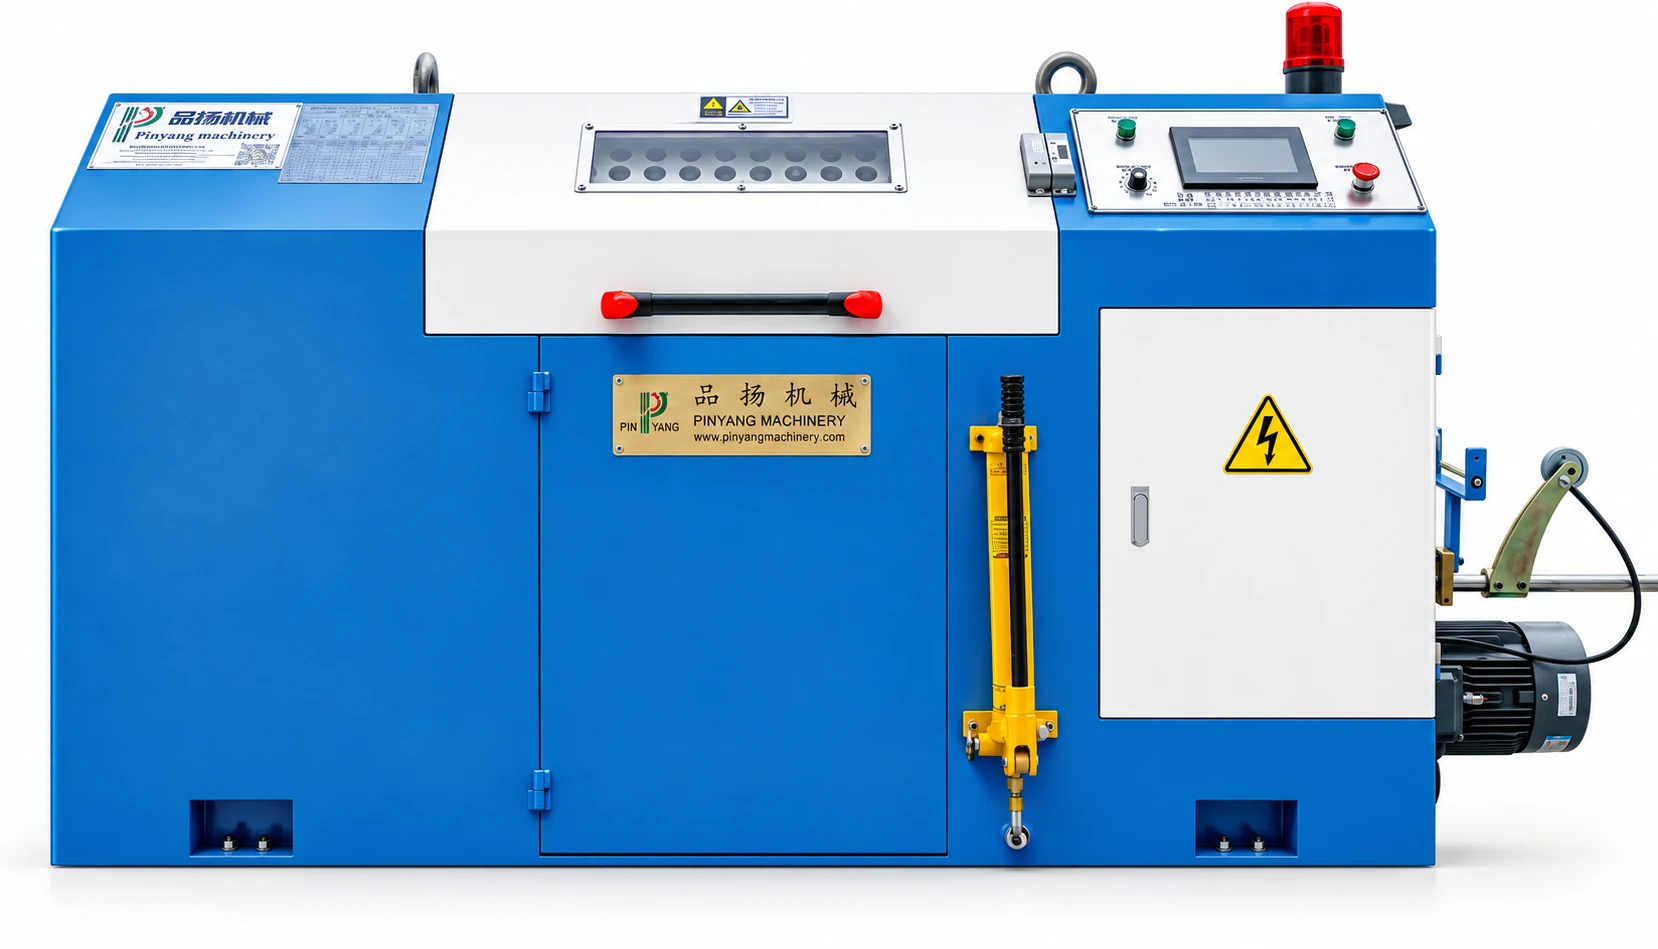
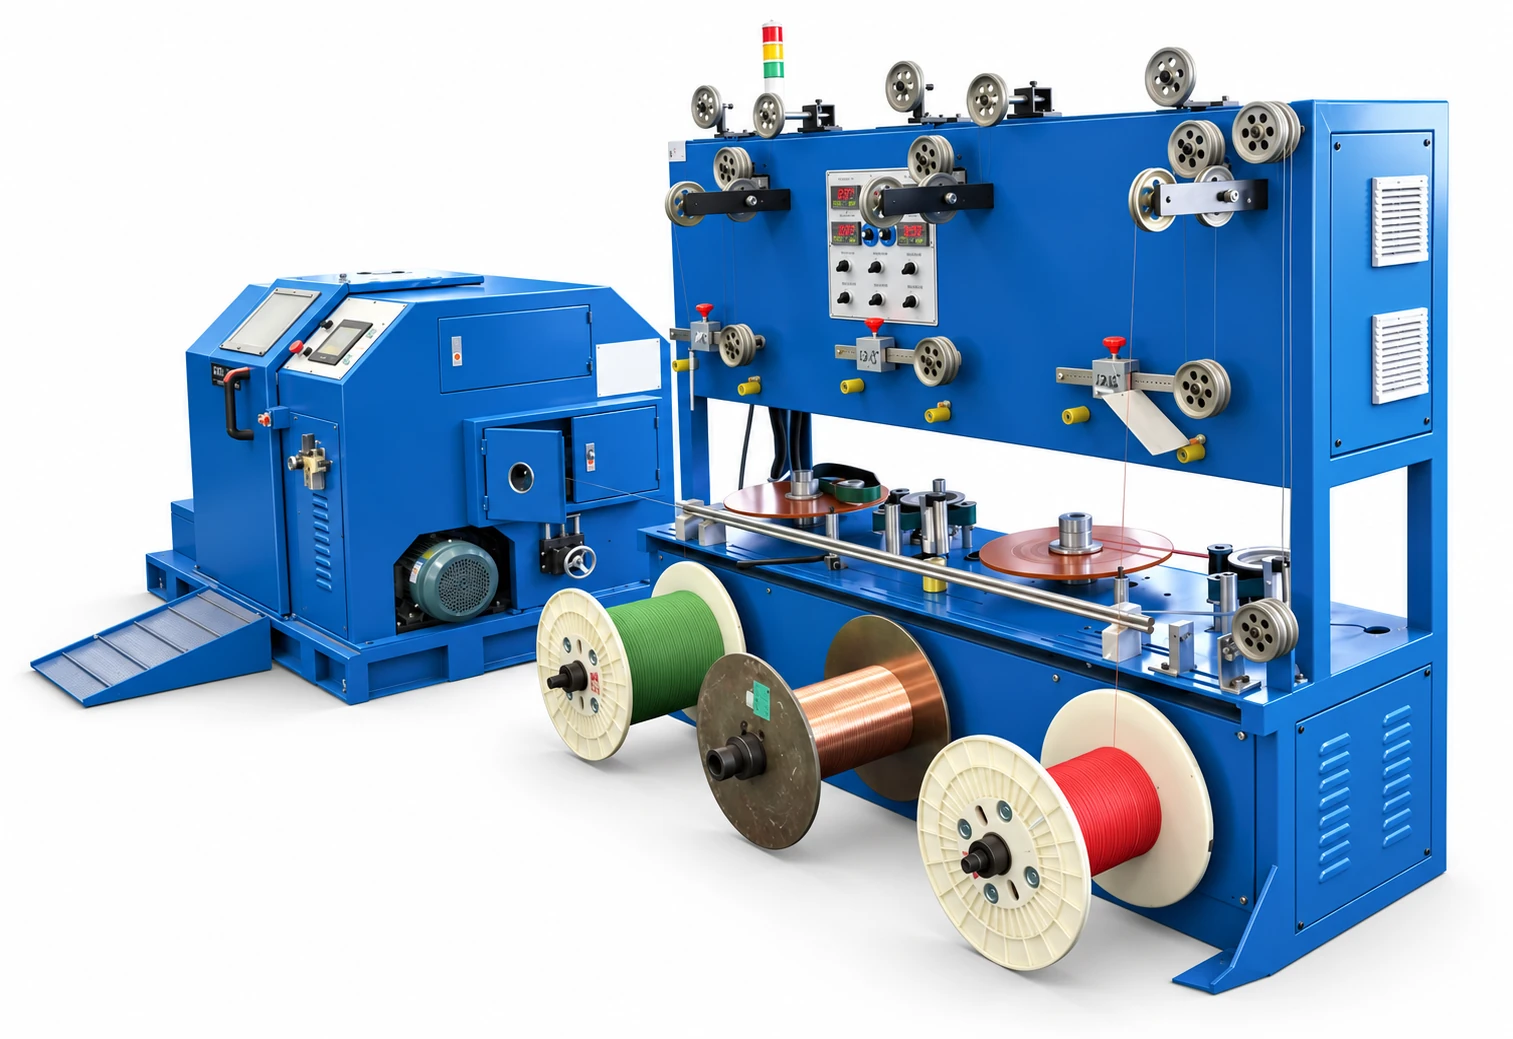
3D visualization: High-speed bunching machine
Catalogue high-speed bunching machineConductor-formation example for the purchased individual wires.
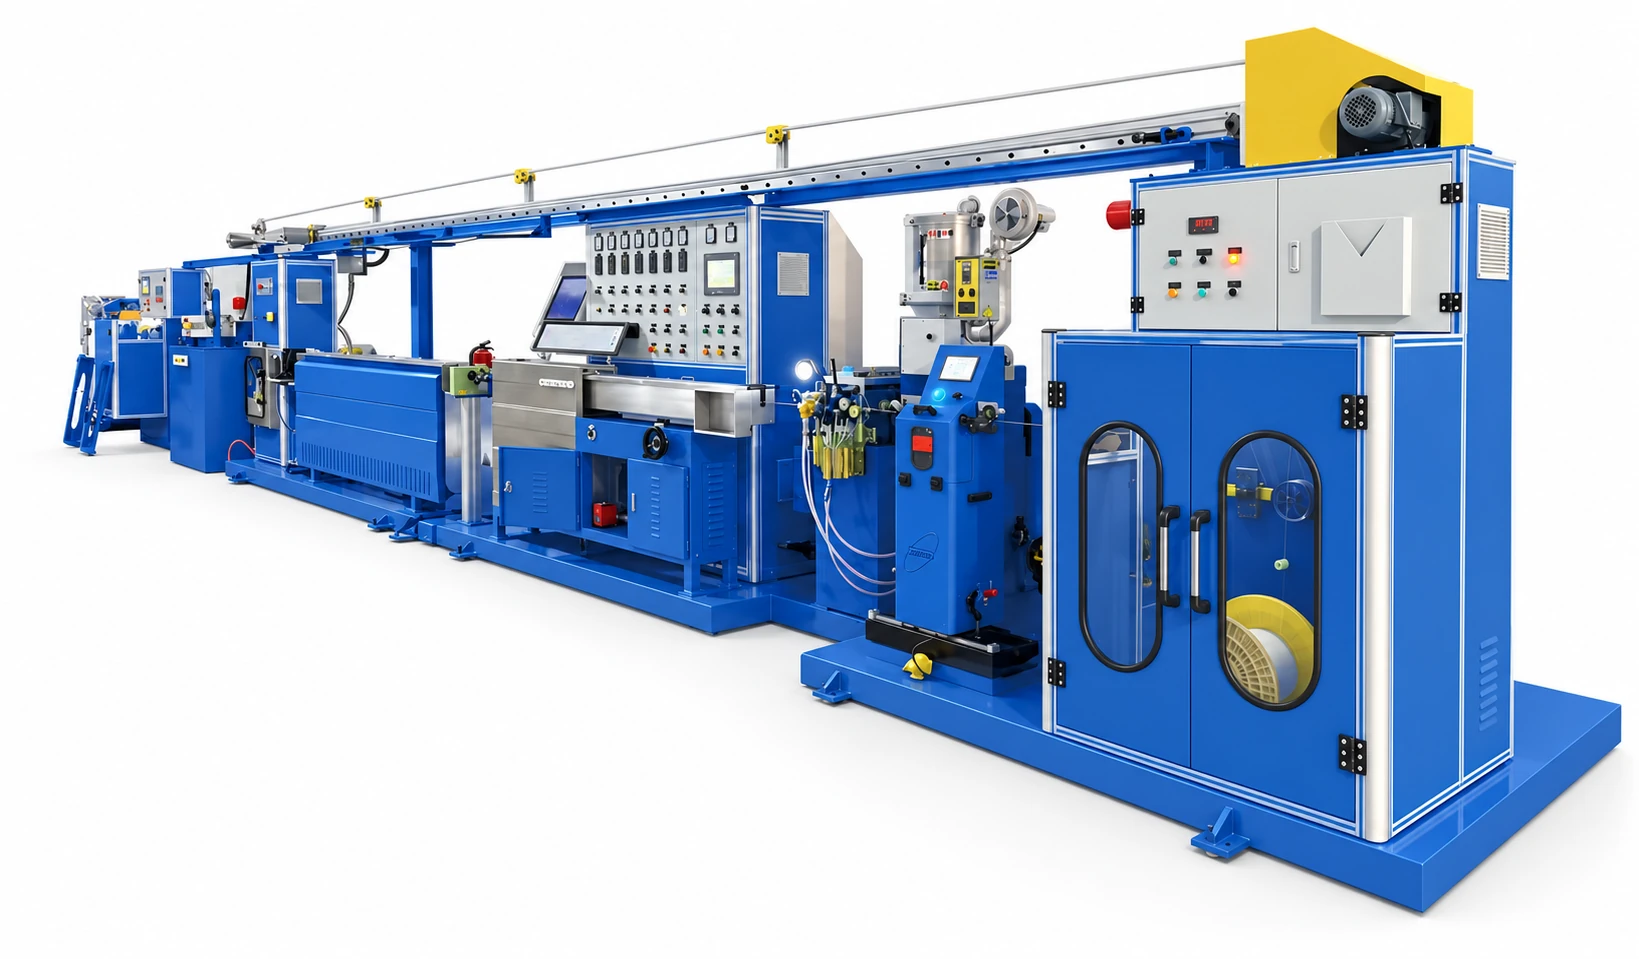
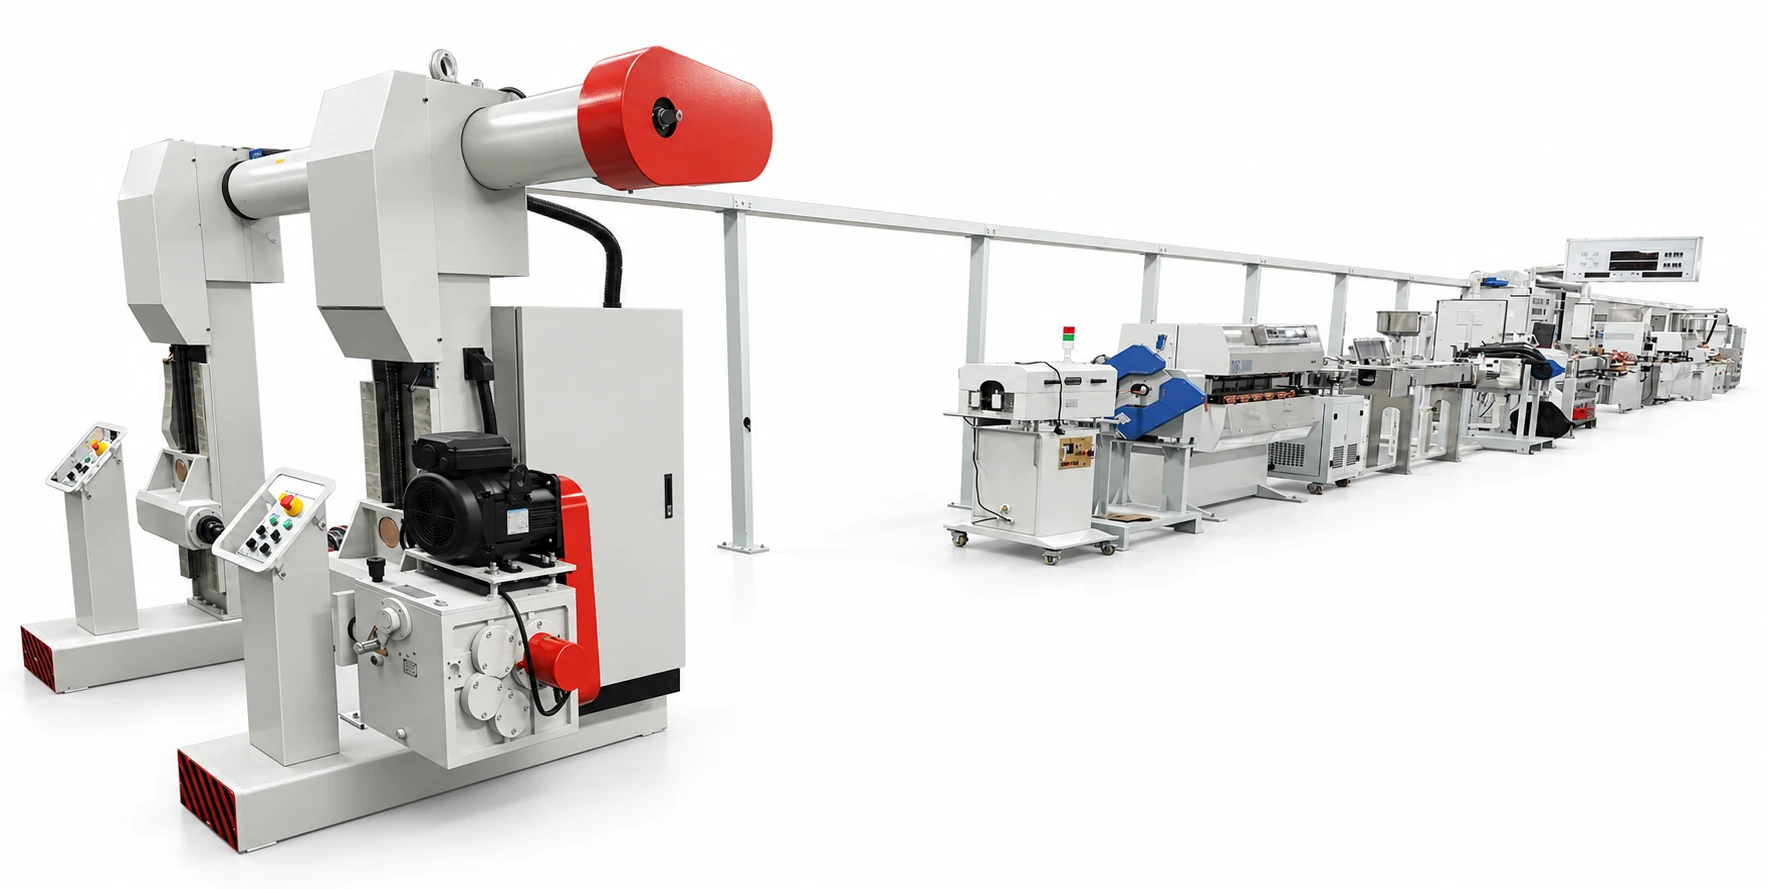
3D visualization: New-energy cable extrusion line shown in the PINYANG catalogue
Catalogue new-energy cable extrusion equipmentRelated insulation-stage context; cord compounds, tooling and dimensions need their own review.
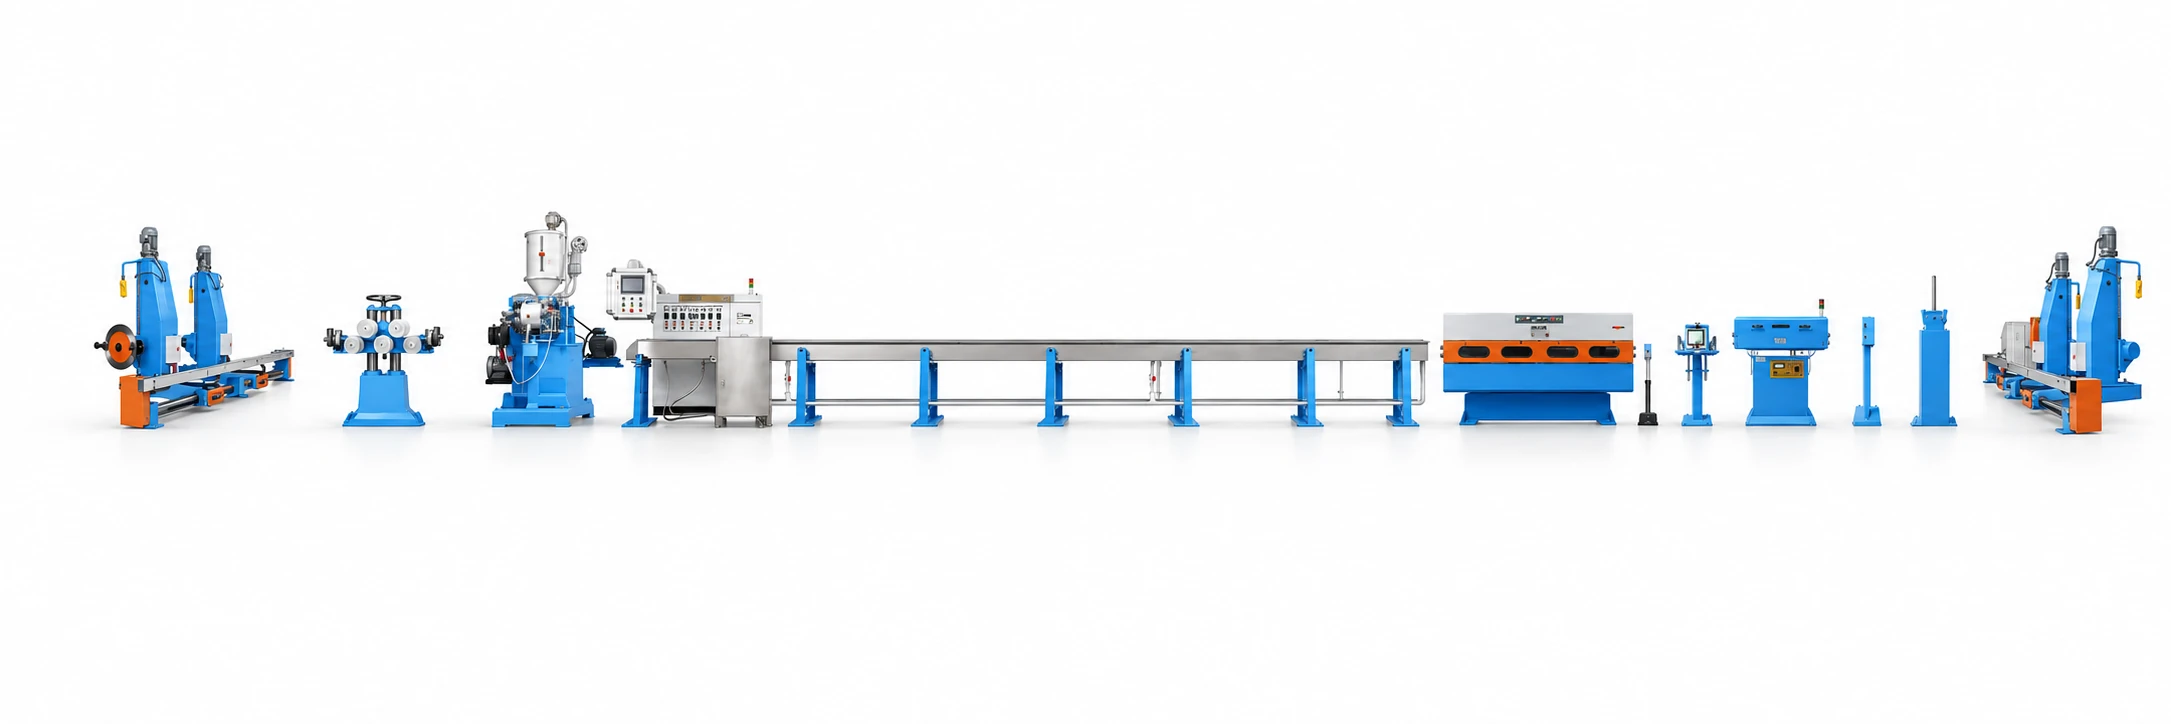
3D visualization: New-energy cable extrusion line shown in the PINYANG catalogue
Catalogue new-energy cable extrusion equipmentRelated extrusion-stage context; confirm the bought-in core arrangement and the cord-sheathing configuration.
Compare the equipment boundary

Buy individual conductor wires

  1. Bunch
  2. Insulate
  3. Arrange cores
  4. Sheath & finish

Bunching → core insulation → assembly where required → sheath → coiling or cutting.

Supply boundary & incoming-material checks
Outside or separately confirmed
Upstream drawing and annealing are outside this initial wire-to-cable scope.
Check the incoming material
Single-wire dimensions, strand count, finished cross-section, wire condition and reels.
Compare the equipment boundary

Buy finished flexible conductors

  1. Insulate
  2. Arrange cores
  3. Sheath
  4. Finish

Core insulation → the specified cable arrangement → sheathing → bulk-cable finishing.

Supply boundary & incoming-material checks
Outside or separately confirmed
Bunching equipment can be excluded when the conductor is purchased ready for insulation.
Check the incoming material
Conductor construction, reels, insulation compounds and the required core dimensions.
Compare the equipment boundary

Buy insulated cores

  1. Review supplied cores
  2. Arrange cores
  3. Sheath
  4. Finish

Arrange or assemble the cores according to the round or flat design, then sheath and finish the cable.

Supply boundary & incoming-material checks
Outside or separately confirmed
Conductor formation and core insulation can be excluded.
Check the incoming material
Core count, sizes, colors, dimensions, incoming quality and the feed arrangement at the sheath process.

This defines a discussion scope. The final equipment list follows the cable drawing and technical review.

Explore the production route

Select a stage to see its role, equipment and the interface to confirm.

3D visualization: High-speed bunching machine
High-speed bunching machine
Power Cord

Conductor formation

Bring individual wires together into the specified flexible or stranded conductor.

Input
Individual conductor wires
Output
Conductor of the required construction

Confirm the interfaceSingle-wire size, strand count, lay, finished cross-section and transfer reels.

3D visualization: New-energy cable extrusion line shown in the PINYANG catalogue
New-energy cable extrusion example
Power Cord

Insulation extrusion

Apply the specified insulation around each conductor. Material and cable geometry determine the configuration.

Input
Prepared conductor
Output
Insulated core

Confirm the interfaceCompound grade, wall thickness, finished diameter, cooling and in-line inspection.

Specified insulated cores
Core arrangement, where required
Assembled cable core
Process schematic — configuration follows the cable drawing
Power Cord

Core arrangement, where required

Assemble the cores or pairs specified on the cable drawing, with the required lay and handling arrangement.

Input
Specified insulated cores
Output
Assembled cable core

Confirm the interfaceCore or pair count, lay, fillers, tape requirements and take-up format.

3D visualization: Power-cable extrusion line shown in the PINYANG catalogue
Power-cable extrusion example
Power Cord

Sheathing & finishing

Apply the outer layer and plan inspection, take-up and the final reel or coil.

Input
Assembled cable core
Output
Sheathed cable in the agreed package

Confirm the interfaceJacket compound, finished dimensions, take-up reels and any separate final testing.

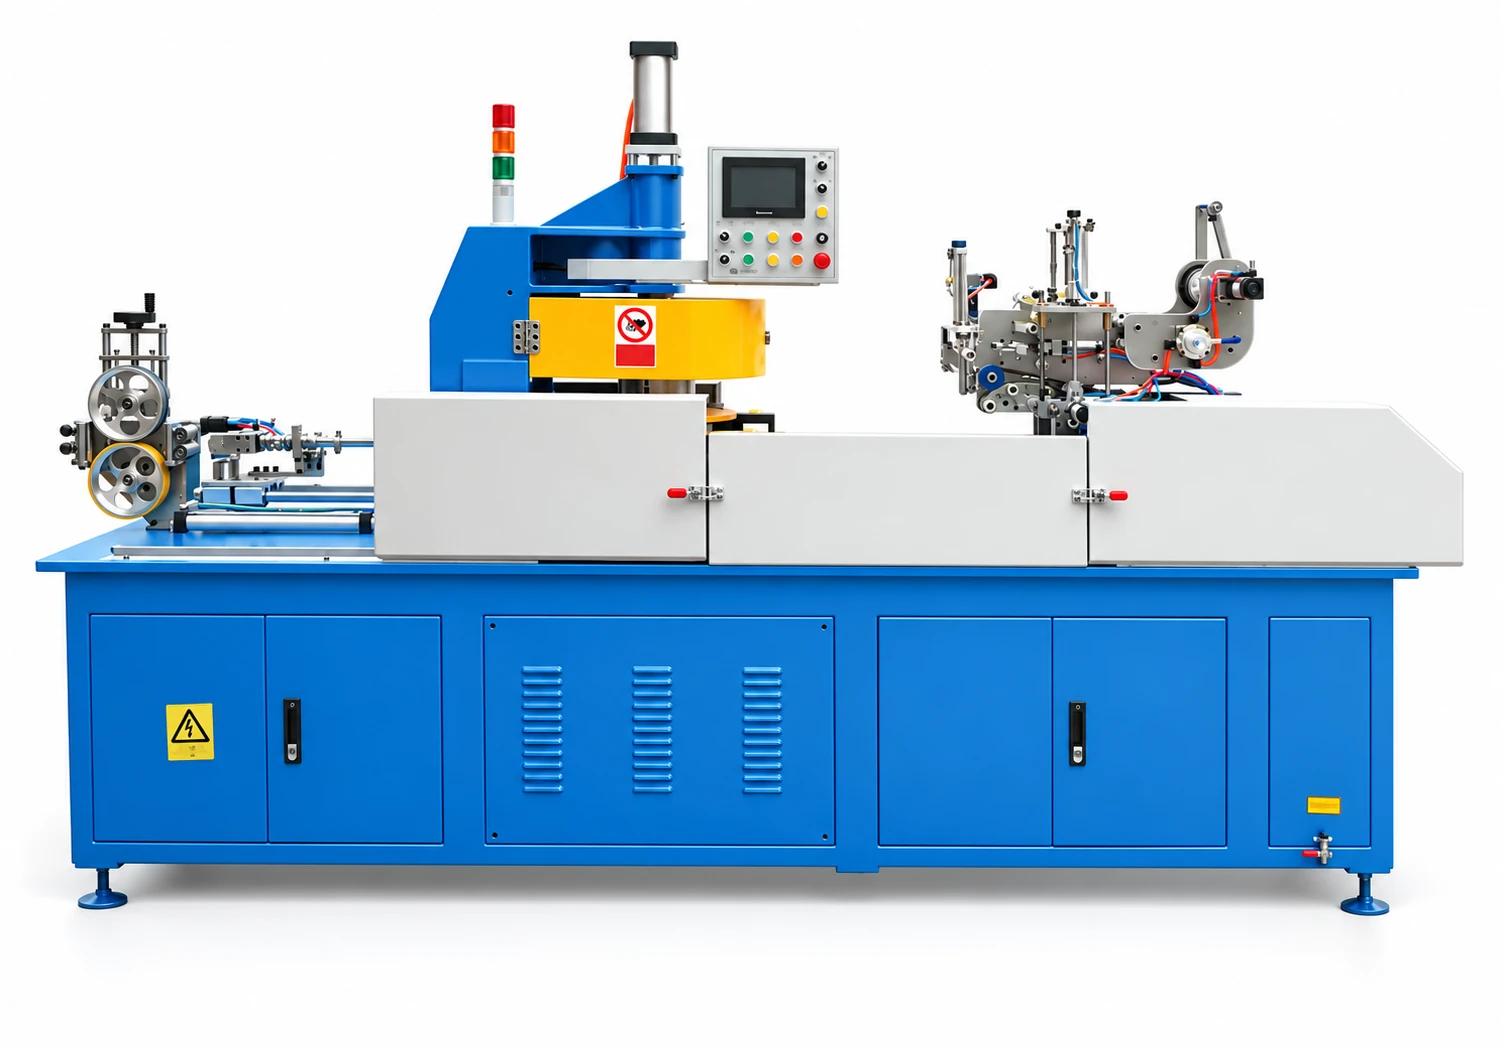
3D visualization: Automatic PLC coiling and wrapping machine
Automatic coiling and wrapping machine
Power Cord

Coiling & cutting

Prepare the cable for the agreed reel, coil or cut-length package.

Input
Finished bulk cable
Output
Cable in the specified package

Confirm the interfaceCable length, coil dimensions and handling. Plug molding and termination are separate scopes.

Compare the construction choices

A different cable structure can change machines, tooling and supply responsibilities. Compare these choices before agreeing the equipment list.

3D visualization: New-energy cable extrusion line shown in the PINYANG catalogue
Catalogue new-energy cable extrusion equipmentRelated extrusion-stage context; the round-cord core arrangement and selected line remain to be confirmed.
3D visualization: New-energy cable extrusion line shown in the PINYANG catalogue
Catalogue new-energy cable extrusion equipmentRelated extrusion-stage context only; this photograph does not verify a flat-cord head or core-feed arrangement.
3D visualization: Automatic PLC coiling and wrapping machine
Catalogue automatic coiling and wrapping machineBulk-cable packaging example; cutting, plug molding and termination have separate scopes.

Round cable construction

Review core laying-up, any fillers or tapes and the sheath arrangement.

What changes

Core count and assembled diameter influence the cabling and extrusion equipment; not every cord drawing uses the same assembly.

Confirm before selection

State the core dimensions, lay, filler requirements and finished diameter.
Flat cable construction

Review how the cores are presented to the extrusion head and how the cable shape is controlled.

What changes

Do not automatically copy a round-cable laying-up stage into a flat-cable route.

Confirm before selection

Provide the cross-section, core spacing, finished width and thickness, compound and package.

Reel, coil, cut length or terminated cord

Take-up, coiling and cutting are selected around the bulk cable and final handling requirement.

What changes

A coiler or cutter does not perform plug molding, termination or completed-cord testing.

Confirm before selection

Define the exact delivered package and list downstream assembly operations separately.

Explore the equipment for this cable

Open an equipment family to compare machine types and reference specifications.

Agree the output, site and acceptance basis

A connected line needs a common specification at every handover. Use these points to test whether the proposed scope is complete.

Production target

Capacity in usable cable or packages

State finished metres per shift and, if relevant, the coil or cut length.

Review the planning details

Compare conductor and core output against the required core count, then account for sheath changeovers and the actual packaging cycle.

Factory interfaces

Color, core and package flow

Plan how insulated cores are identified, stored and matched before sheathing.

Review the planning details

Coordinate take-up or coiler access with the next operation, especially when bulk cable moves to a separate plug-assembly area.

Acceptance plan

Trial and acceptance

Use the agreed conductor construction and insulation and sheath materials.

Review the planning details

Confirm cable shape, layer dimensions, required cable tests and package quality; plug and termination acceptance belongs to the downstream assembly scope.

Put responsibilities in writing

Identify who provides trial materials, utilities, reels, testing and any external process. Agree how results will be recorded and what must be resolved before acceptance.

Compare investment on the same scope

A useful budget separates the machines from plant preparation, external processing and start-up requirements. No standard package price can replace a defined cable specification.

Configuration and purchasing choices that change the budget
DecisionWhat enters the scopeHow to compare
Core preparationBunching, insulation configurations, color changes and the planned core-size range.Use the same conductor construction and material grades when comparing offers.
Cable shape and packageCore arrangement, sheath tooling, reel or coiling equipment and any cut-length requirement.Distinguish cable-making equipment from plug molding, termination and completed-cord tests.
Phased purchasePurchased conductors or insulated cores can be considered before adding upstream processes.Review the future production mix, incoming quality, reel formats and space for those later operations.
3D visualization: Automatic PLC coiling and wrapping machine
Catalogue automatic coiling and wrapping equipment

Use the catalogue as a starting point

The catalogue includes coiling and wrapping equipment with cable and coil-size reference ranges, giving a basis for reviewing the finished package.

A compatible cable diameter alone is insufficient: flexibility, length, coil geometry and handling also need review. The equipment is not plug-making evidence.

Prepare your line-planning requirements

Core construction

Supply the core count, conductor structure and individual core dimensions.

Material system

Confirm insulation and sheath materials for the intended product.

Cable shape & dimensions

Finished geometry and dimensions guide the extrusion review.

Downstream operations

Plug molding, termination and assembly testing require their own scope.

Application questions

Is plug molding included in a cable line?

Not automatically. The equipment on this page concerns manufacturing the cable. Plug molding and final cord assembly should be identified as separate project needs.

Can the line include coiling and cutting?

The catalog includes coiling and cutting equipment. Selection depends on the cable, finished length and packaging format.

Can equipment be selected for several cord sizes?

A defined product range can be reviewed together. Share the smallest and largest constructions and the planned production mix.

Does a flat power cord need the same cabling stage as a round cord?

Not necessarily. The core arrangement and extrusion-head feed follow the drawing. Provide core spacing, finished width and thickness for a flat design, or lay and assembled diameter for a round design.

Should output be compared in metres or finished coils?

State both if you sell coils or cut lengths. Cable production and packaging have different operating cycles. Agree the package length, dimensions, handling and required completed packages alongside the cable output target.

Your Project Brief

Share the cable you want to make and the scope of your project.

Company & project details (optional)

Prepare and download a project brief locally. No inquiry is sent.

Your Project Brief

Review your details before downloading.

Prepared locally. Not sent.